

OEE calculation : how to calculate the OEE
The calculation of the OEE is the first step in the search for the optimal performance of the means of production. It is a daily concern for companies. In this sense, the OEE is the key performance indicator to measure the productivity of a means of production and a plant.
What is the OEE ?
As its name indicates, the Overall Equipment Effectiveness (OEE) is an indicator that provides a synthetic view of the performance of the means of production concerned.
In 2002, CETIM and AFNOR specified and standardized the calculation of the OEE. The standard NF E 60-182. This standard defines in particular that the improvement of the industrial performance passes by three objectives :
- Reduction of production downtime
- Elimination of human and material dysfunctions
- Scraps reduction
Measuring the OEE is a fundamental practice for those who wish to have a complete and precise vision of the productivity of their production tool. Through this indicator, you get crucial information. It indicates how to improve your manufacturing process, by identifying and qualifying losses.
OEE calculation : Times status
In order to make the OEE calculation more accurate and understandable, we use “times status”.
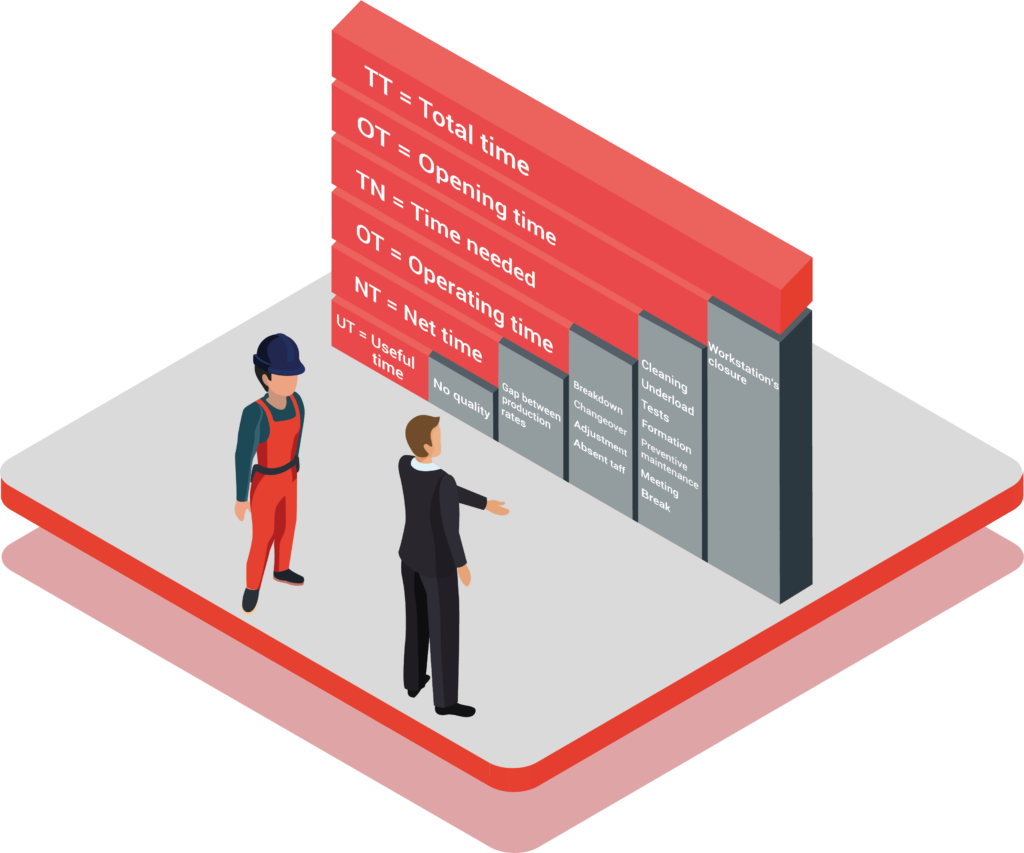
Total time
It is the time of possession of the means of production. Theoretical time during which the means is usable to produce (it is 24h for one day, 168h for one week…). It is thus made up of all the other times status.
Scheduled Time
Opening time of the shop floor during which the means of production can be used.
ST = total time – plant closure
Planned production Time
Reference time during which the means of production is engaged to produce.
PT = scheduled time – planned downtimes
Operating Time
Time during which the means of production has actually produced.
OT = planned production time – unplanned downtimes
Net Operating Time
Time during which the means of production produces goods within the standard cycle time.
NOT = Operating time – Performance loss
Fully Productive Time
Time during which the means of production produces goods in the respect of the quality criteria. This is not measurable but calculated by multiplying the number of good parts with the standard cycle time.
OEE calculation : The different ways to do it
There are several ways to calculate the Overall Equipment Effectiveness, depending on the available elements.
OEE calculation by the ratio of times status
First, the most basic formula for calculating OEE is the ratio of Fully productive time (time during which good parts are produced at the right rate) to Planned time (organizational time for engaging resources).

But this formula is opaque as to the real health of the production. While the Planned Production Time is easily accessible (Scheduled time – Planned downtimes), it is more complicated to know the standard cycle time (Fully productive time = Good quantity x standard cycle time).
However, this notion is not necessarily present in all manufacturing processes.
OEE calculation by quantities
Secondly, the calculation of the OEE can be done with the ratio between the good quantity realized during the Fully productive time and the theoretically realizable quantity during the Planned production time.
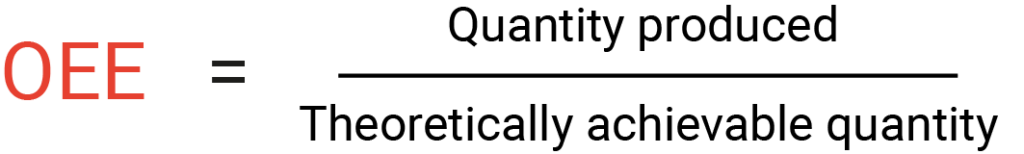
This calculation highlights the difference between the quantity of units that can be achieved and the quantity actually achieved. But while it is quite valid, it does not provide information on the three factors related to losses: Quality, Performance and Availability.
OEE calculation by performance indicators
Much more than a calculation, it is a health status.
The advantage of calculating OEE through this calculation is that it provides a complete health status of the means of production, shop floor and plant by relating the three internal factors explaining losses: Quality, Performance and Availability.
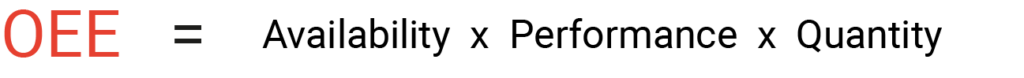
These three factors are determined by measurable indicators:
1 Availability
The availability rate measures all the events that interrupt production and that have a sufficiently long duration to be useful to determine the reason. Firstly, these downtimes can be internal causes. That we call downtimes (machine stoppage, malfunction of tools, adjustment). Secondly, external causes. The induced downtime (understaffes, lack of parts, lack of energy, upstream or downstream issues).
In addition, the availability rate is equal to the ratio between the operating time of the means of production and its planned production time (commitment time).

Availability can also be the ratio of actual operating time and the planned uptime. Likewise, actual operating time can be obtained either by direct measurement or by measuring all downtimes and subtracting them from the planned production time.
2 Performance
In any manufacturing process, there are reasons why it is likely to operate at a rate, speed or cycle time below or above the nominal or standard value (rate variation). This is called actual performance. It is calculated as the ratio of the net time to the operating time of the equipment.

It’s also about comparing how many units you produce and how many you could. This is at the maximum or rated speed for the time the means of production was actually running.
The produced units correspond to everything that was produced including scrap. To calculate what could be produced, it simply needs to multiply the actual operating time by the rate.
3 Quality
This rate allows us to judge the quality of the production, it corresponds to the ratio between the good quantity and the realized quantity. This ratio allows us to know the quantity of “non-quality”, called scrap. These scraps are defined as all the products that do not meet the quality criteria. They are then losses of material and time.
It can be calculated either by times or by quantities :
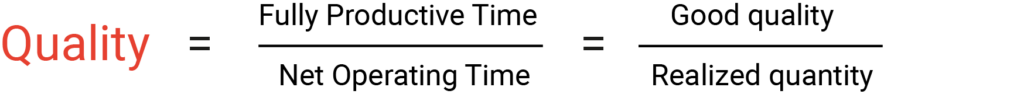
Final OEE calculation
Thus to calculate the OEE of a means of production by the indicators, it is enough to make the product of the three rates defined previously.
OEE = Availability x Performance x Quality
Firstly, this OEE calculation allows to trace and quantify the quality of a production. Secondly, it allows the identification of losses and areas for improvement.
Good to know:
It is possible to express each of the three rates that make up the OEE in parts ratio rather than time ratio.
1 Availability

2 Performance

3 Quality

Thanks to IIoTs and all the data collected, Astn’go automatically measures the OEE in real time. It identifies all the causes of non-OEE in order to eliminate them through the implementation of action plans. Astn’go is the support for continuous improvement processes that helps you make decisions. It frees up time for you and your operators to focus solely on high value-added actions.
To go further
Thus the measurement of the OEE allows to launch many improvement projects. For example, SMED and visual management projects, with the aim of rapidly improving your competitiveness.
Sources:
Practical guide “The OEE performance indicator” published by CETIM (https://livre.fnac.com/a3746090/Ayel-Le-TRS-indicateur-de-la-performance)