

Machine signal consideration
1. General information about signals
Count
It is necessary to wire a contact to the IIoT that indicates the end of production of a manufactured unit—this is referred to as “Top cycle.”
Consideration of the production statement
This signal must correspond to the general status of the production equipment. The signal corresponds to an input (0 = downtime/1 = production) on the IIoT module of the following type:
- On–off-control signal: activation example of a 0/1 relay output that is connected directly to an IIoT input (IIoT in Dry mode).
- PLC: output retrieved directly from the PLC output terminal block (IIoT in Wet mode).
- From a sensor corresponding to a counting cell.
The production statement (on/off) can :
- Be provided directly from the equipment.
- Be a combination of several statuses on a set of information constituting the equipment to be monitored.
- Be provided using an external element representing the status of the equipment: for example, light columns (verrines) that allow a status to be retrieved (existing signals) without necessarily having to access the equipment to take the information into account..
2. Robot
Count
- The signal can come directly from the robot or from a detection cell, for example on an evacuation conveyor.
- This signal corresponds to a pulse. On the rising edge, our acquisition will count +1 unit.
- It is possible to relay the information or directly provide an automatic output.
Consideration of the production statement
- The robot is operational
- No intrusion into the area
- Management of production cell equipment (e.g., conveyor systems)
3. Rotary press
Corresponds to a printing or cutting machine.
Count
- Possibility of retrieving the count on an encoder wheel (pulse). In Astn’go, it is possible to define the number of pulses to produce, for example, 1 meter.
Consideration of the production statement
- The status is linked to the presence of counting on the rotary press.
- An independent input can be wired to determine whether the equipment is on or off
4. Packaging line/Production line/Manufacturing line
Machine for tracking and counting items (such as bags, cases, etc.) individually or in groups.
Count
- Top cycle counting input: good part
- Entrée de comptage Top cycle : rebut
Peut correspondre à une cellule de comptage sur la ligne de conditionnement ou à une information disponible depuis une sortie automate. Le signal peut être relié directement au module IIoT ou être relayé électriquement via un relai et permettre la mise à disposition d’un contact “sec” de comptage.
Prise en compte de l’état
- L’état est lié à la présence de comptage sur la ligne
- Top cycle counting input: scrap
5. Numerical Control (NC)
In general terms, we will discuss all machine tools that enable the machining of parts.
Count
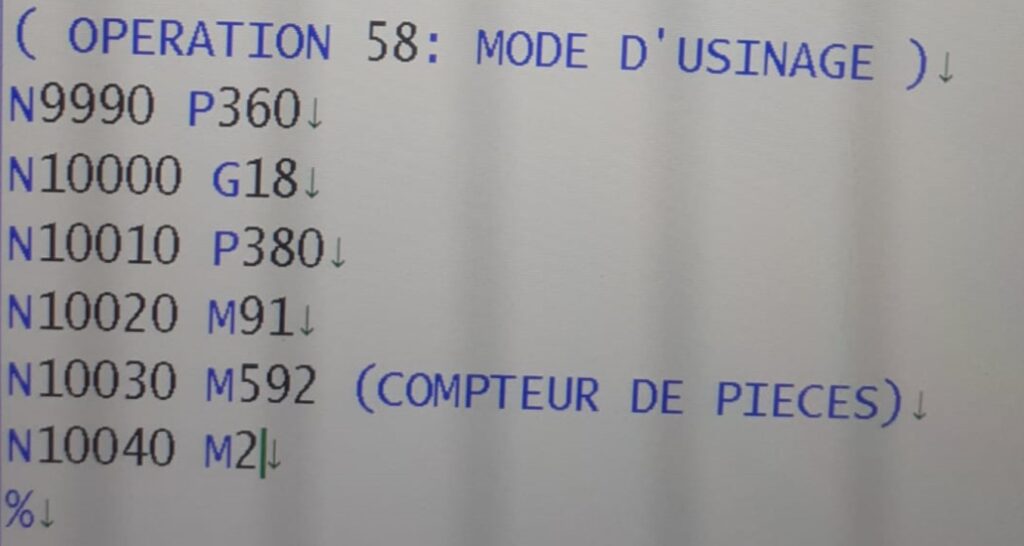
- Top cycle counting input: good part.
This information corresponds to an M2 or M30 function in the NC program. In the program, before this M1 function, it is possible to add an M intrusion that will enable the activation of a relay output:

Consideration of the production statement
- Taking into account additional information “Cycle in progress” which corresponds to the machining phase of the part. This information can be taken into account using the intrusion of the NC program M0 which corresponds to the pause state before the start of a new cycle.
- The end of a production cycle can also be taken into account to consider that a part has just been finalised.
6. Press
The term “press” refers to machines used for injection molding (plastic/metal) or cutting (stamping press). For injection molding, counting can correspond to molds—in this case, it is possible to define a number of parts produced per mold (information related to the operation, reference, or equipment).
Count
- Top cycle counting input: good part individually or per mold
- Top cycle counting input: rejected part individually or per mold
Le The signal can be connected directly to the IIoT module or relayed electrically via a relay, providing a “dry” counting contact.
On injection molding machines, it is possible to use the “Opening” or “Closing” mold information to count the number of molds produced. During the production process, it may be necessary to perform empty opening/closing movements. In this case, information on the status of the machine can also be added to the IIoT to avoid counting these empty movements.
It is also possible to use the “Top dosing” information, which allows the supply of material to be combined with the completion of a molded part. This solution makes it possible to exclude empty molded parts from the count. Finally, using programming languages specific to each press, it is possible to activate an available output at the end of the cycle and connect it to the IIoT.
Consideration of the production statement
- The production statement is linked to the presence of production.
he production statement is linked to the presence of production.
An independent input can be wired to determine whether the equipment is running or not.